


Internationally Approved Product
 ULListed
 FMApproved
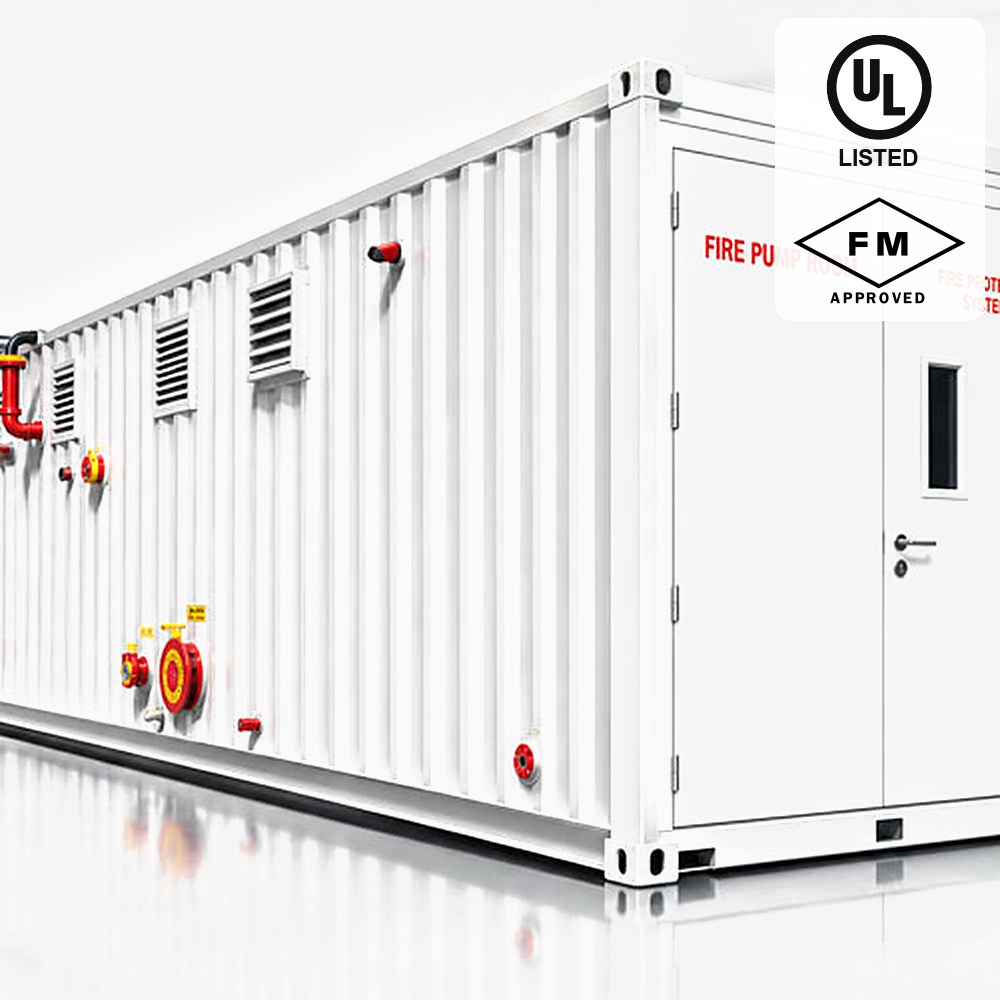
Ready-to-Install Fire Pump Solution
A container pump room is a pre-assembled and ready-to-install fire pump solution where fire pumps, controllers, and necessary accessories are mounted on a common base frame. The system simplifies the on-site installation process with its pre-wired connections and auxiliary equipment prepared in a factory environment.
The container pump room consists of fire pumps, controllers, accessories, and a common base frame. The fire pumps include the pumps used in the system, while the electric, diesel, and jockey controllers ensure the control of the system. Accessories required by NFPA 20 are mounted on pre-prepared connection pipes. All these pieces of equipment are assembled together on a common base frame.
The necessary wiring between the controllers and the system is completed at the factory prior to shipment. The automatic air release valve, casing relief valve, suction gauge, and discharge gauge are mounted on the fire pumps. Other accessories are mounted on the pre-prepared connection pipes as required by NFPA 20.
Pressure sensing lines are pre-installed to the Electric, Diesel, and Jockey Controllers in accordance with NFPA 20 requirements.
To ensure performance in accordance with design requirements, the systems undergo performance testing at the factory in compliance with UL, FM, and NFPA standards.
To complete the installation of these pre-engineered and ready-to-install systems, it is sufficient to grout the structural base and connect the suction and discharge piping as well as the incoming power.
UL and FM certified components are used in container pump room systems. The systems undergo performance testing at the factory in compliance with UL, FM, and NFPA standards. The engineered packaged pump meets the requirements specified in the Packaged Fire Pump Assemblies section of NFPA 20.


